
Overview of Short-run, High-mix Microelectronics Packaging
Short-run, high-mix microelectronics packaging presents a unique automation challenge. Manufacturers need the quality and repeatability benefits of automation, but frequent product changeovers can make conventional high-volume solutions impractical. A successful high-mix automation strategy begins with a standardized material-handling platform.Properly designed transport carriers and magazines allow multiple package types to move reliably between process work cells while minimizing equipment changeover. These systems can be integrated into a wide range of processes:
-
-
-
Die Attach
- Wire Bonding
- Inspection
- Laser Marking
- Functional Testing
-
Final Packaging
-
-
By standardizing the method used to transport products throughout the manufacturing process, manufacturers can reduce operator intervention, improve process consistency, enhance product traceability, and create a scalable platform for future automation. Whether implemented within a standalone work cell or a fully integrated production line, transport carriers and magazines enable efficient product flow between manufacturing operations while supporting short-run, high-mix production requirements.
This guide examines the first two foundational elements of that automation strategy: the package transport carrier and the carrier transport magazine.
Step 1: The Package Transport Carrier
The package transport carrier is the foundation of any short-run, high-mix automated assembly process. By leveraging edge-belt conveyors, it efficiently moves packages through various process work cells, ensuring seamless and reliable automation.Selecting the right carrier is essential for maintaining precision, repeatability, and overall process efficiency. Factors such as size, material, and design should be carefully assessed to optimize workflow, enhance handling, and ensure long-term system performance.
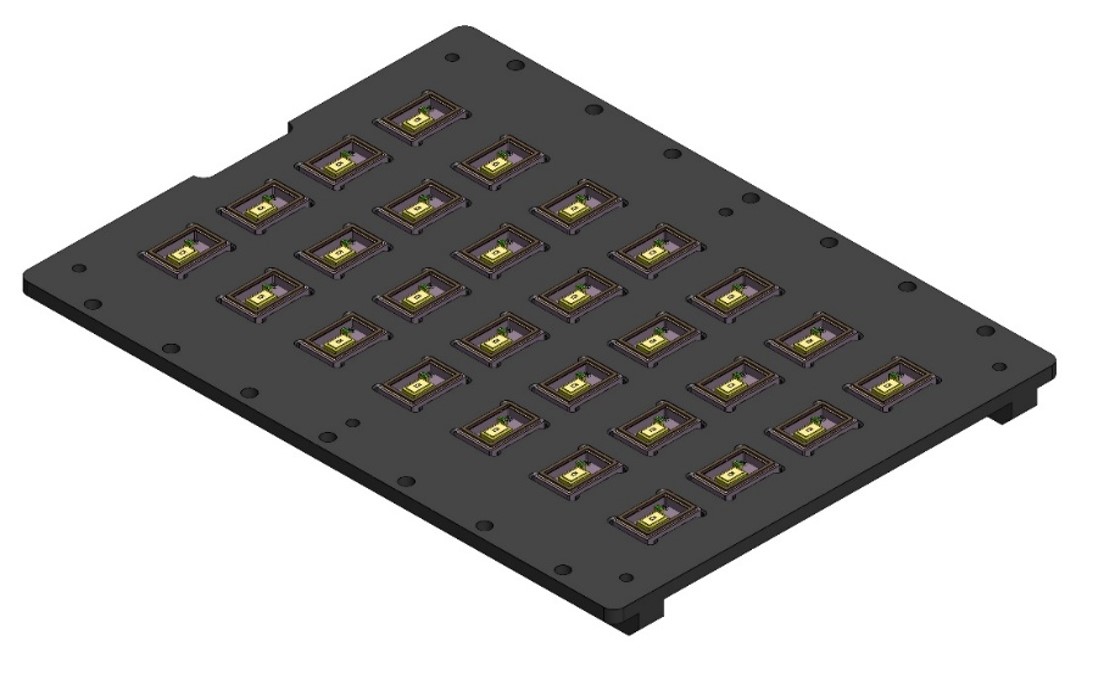
Machined Metal Carrier
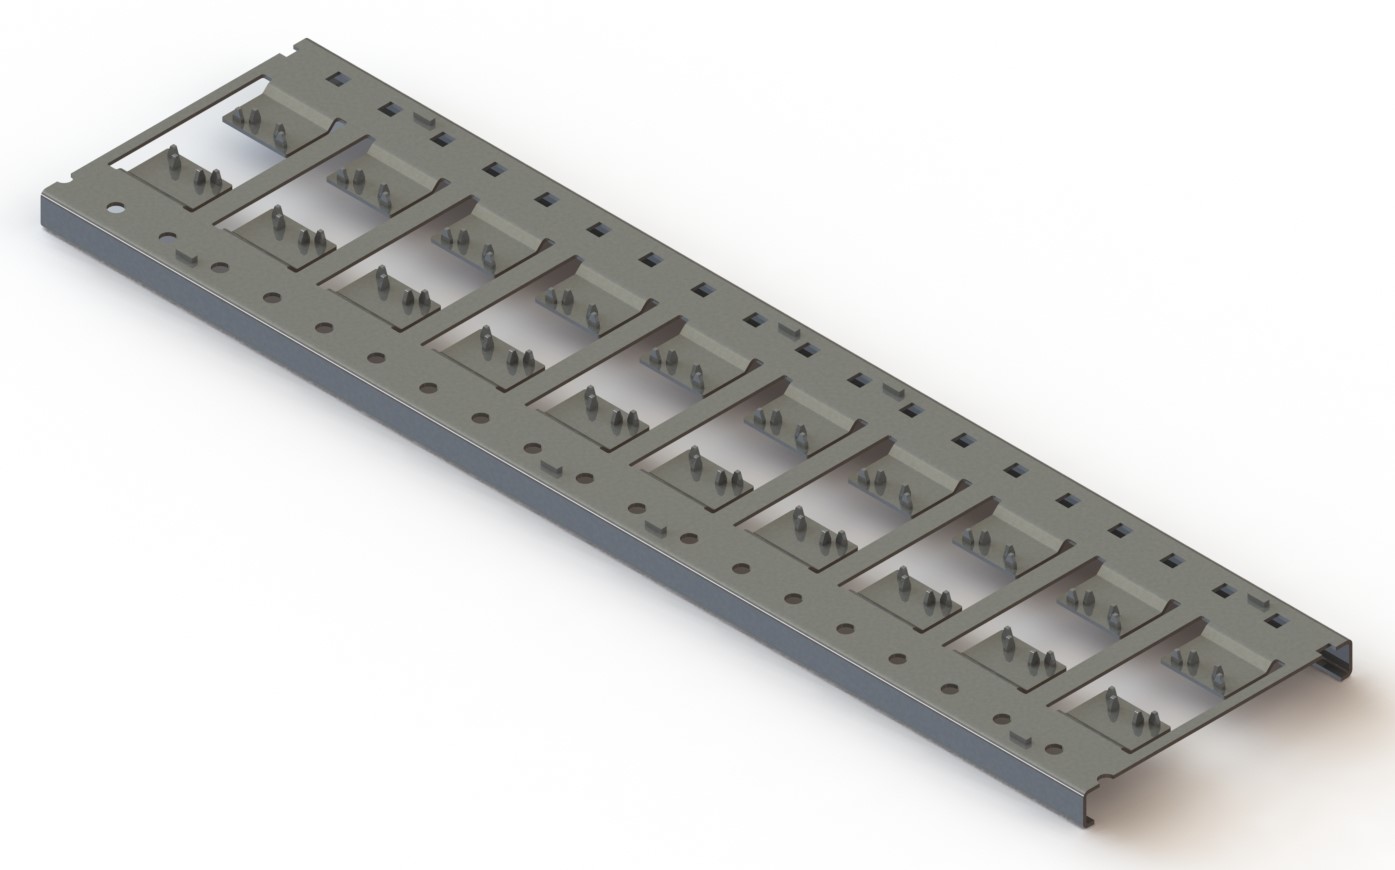
Sheetmetal Carrier
Carrier Design Considerations
Carrier Size
To ensure consistency and efficiency, all products to be conveyed should be assessed, and a standardized carrier size should be selected to accommodate the full range of products. Standardizing the carrier width and length minimizes change over time between different product types, improving overall process efficiency. The size of the largest and smallest packages determines the required width of the carrier. Industry standard carrier length is 12 in. but shorter ones can be used if other circumstances require it.
Parts per Carrier
Maximizing the number of parts per carrier seems like an efficient approach, but it comes with trade-offs. Here are some key considerations:
-
-
- Clamping Force Limitations
Processes like heavy wire bonding require high clamping forces, which may be problematic if too many parts are loaded. - Work Order Size
If the order size is small, it might not be efficient to use a high-capacity carrier if it results in partially filled loads. If the process relies on vacuum clamping, open or empty positions in the carrier can cause problems, potentially reducing stability and process reliability.
- Clamping Force Limitations
-
Carrier Type
Carriers are typically manufactured in two types:
1. Sheet Metal Carriers
Progressive dies are utilized to fabricate carriers from stainless steel sheet metal in an automated die process.
-
-
-
-
-
- Advantages
Ideal for high-volume production, offering the lowest cost per unit.
- Disadvantages
High non-recurring engineering (NRE) and tooling development costs make it less viable for low-quantity applications.
- Thermal Considerations
When exposed to thermal cycling, they may warp over time, leading to feeding jams and requiring rework or replacement. - Accuracy
These carriers use tabs for package positioning, which may not provide the precision required for certain assembly processes.
- Advantages
-
-
-
-
2. Machined Metal Carriers
CNC milling equipment is utilized to manufacture carriers from various materials. For ESD safety, conductive materials and coatings should be used in most cases.
-
-
-
-
-
- Advantages
Ideal for low-volume production, with lower NRE and tooling costs compared to sheet metal stamping.
- Disadvantages
Higher per-unit cost due to increased manufacturing cost.
- Thermal Considerations
Machined carriers resist warping even when subjected to thermal cycling. Typically, they will remain flat and precise for many years of use.
- Accuracy
These carriers can be machined to tight tolerances, allowing for precise package positioning.
They also enable the integration of locating and clamping features for enhanced stability.
- Advantages
-
-
-
-
Conclusion
For most short-run, high-product-mix applications, machined carriers are preferred due to their lower upfront costs, extended lifespan and design options compared to sheet metal carriers.
Step 2: The Carrier Transport Magazine
The carrier transport Magazine holds multiple carriers in slots, facilitating the automated loading and unloading of products into and out of assembly cells or an integrated line.
Unprocessed product on carriers are loaded into the magazine slots and placed into an upstream Magazine Unloader system that automates the feeding process.
Once processed, carriers are transferred into a downstream magazine via an automated Magazine Loader.
By integrating magazines with automated unloaders and loaders, manufacturers can streamline the feeding of carriers into individual work cells or along an automated production line, enhancing efficiency and reducing manual handling.

1130U / Work Cell / 1130D
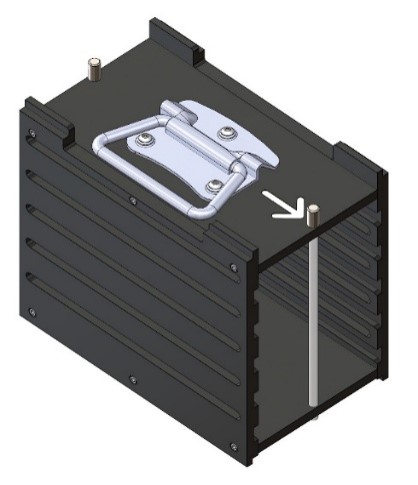
Custom magazine with slots for air flow and pins for containment when transporting.
Magazine Design Considerations
Magazine Size
The magazine size is determined by the carrier dimensions. Standardizing carrier sizes allows Magazine Unloaders and Loaders to maintain a consistent configuration, eliminating the need for changeovers. The magazine's slot capacity depends on the height of the parts and the total weight of a fully loaded magazine. This should be carefully managed to prevent ergonomic issues of operators moving the magazines.
Thermal Cycling
Some users incorporate batch ovens for curing processes which must be considered when designing and manufacturing magazines. If using a convection type oven, then slots or holes to increase airflow is a crucial component.
Magazine Types
1. Sheet Metal Magazine
This type is manufactured using sheet metal fabrication methods, where parts are cut, formed, and assembled using welding or rivets.
-
-
-
-
-
- Advantages
Ideal for high-volume production, offering the lowest cost per
unit. Lightweight and allows for easy integration of airflow features for
thermal cycling.
- Disadvantages
Less rigid, leading to a shorter lifecycle and potential for
jamming
. - Thermal Considerations
Deforms over time when exposed to thermal cycling, reducing lifespan.
- Advantages
-
-
-
-
2. Extruded Magazine
Constructed from extruded aluminum, these magazines are available in fixedsizes:
3.1 x 12, 4.3 x 12, and 5.4 x 12.
-
-
-
-
-
- Advantages
Cost-effective if the standard sizes meet requirements.
- Disadvantages
Requires secondary operations for airflow slots or additional features. Includes stacking features but lacks interlocking, leading to movement when feeding carriers.
- Thermal Considerations
Withstands thermal cycling, but adding airflow features significantly increases cost.
- Advantages
-
-
-
-
3. Machined Magazine
Machined from solid material, offering maximum customization for size and features such as airflow slots and stacking capabilities.
-
-
-
-
-
- Advantages
Best option for custom sizes and features. Cost-effective for smaller production quantities. - Disadvantages
Highest cost per unit.
- Thermal Considerations
Excellent resistance to thermal cycling.
- Advantages
-
-
-
-
Magazine Conclusion
For most short-run, high-product-mix applications extruded magazines are the best option if a standard size fits and thermal cycling is not required.
For custom sizes and thermal cycling needs, machined magazines are the preferred choice.
After finalizing your Transport Carrier and Magazine configurations, automated material handling is essential for efficiently moving products through the assembly process.
At the upstream and downstream points of your assembly cell or integrated line, Magazine Unloaders (upstream) and Magazine Loaders (downstream) play a crucial role in automation.
By incorporating the appropriate magazine handling system, you can streamline your process, improve efficiency, and reduce manual labor.
Martek Automation's Magazine Handlers
We offer multiple models to fit varying capacity needs:
High Capacity:
1130U/D
High Capacity Magazine Handlers
Handles multiple magazines

Medium Capacity:
1500U/D
Small Footprint
Magazine Handlers
Supports two magazines
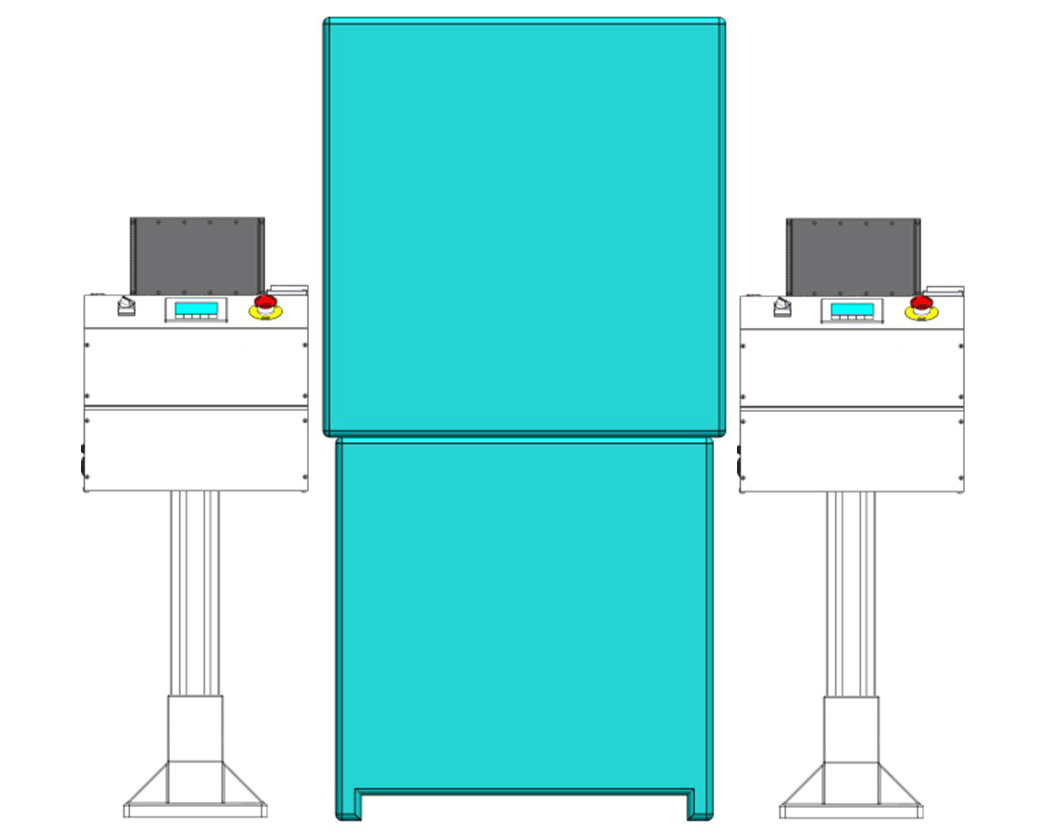
Single Capacity:
SM500
Single Capacity Magazine Handlers
Designed for a single magazine
* Product page coming soon